

Mould Specifications
|
Mould name |
770L wheelie bin Mould |
|
Product material |
Virgin high-density polyethylene plastic |
|
Product Dimension(L*W*H) |
1 250,00 x 760,00 x1 265mm |
|
Volume |
1,202 m3 |
|
Product Weight |
46kg |
|
Mould material for cavity &. Core |
C45, P20 |
|
Mould base |
C45 |
|
Injection system |
Hot runner open gates |
|
Suitable injection machine |
4000T |
|
Mould size |
1850x1300x1900mm |
|
Mould lifetime |
More than 300,000pcs |
Introduction
The Wheelie Bin Mould is a special injection mold for manufacturing wheelie bins. It injects the plastic raw material into the mold cavity through the injection molding process, and after cooling and shaping, a complete wheelie bin is generated.
Manufacturing process
1. Mold design
According to the product size (1250x760x1265 mm) and weight (46 kg), design an accurate 3D model. Based on the hot runner open gate system, design the gate layout to ensure uniform material filling.
2. Mold material processing
Cut the mold material (C45, P20) to the appropriate size using a sawing machine or CNC cutting machine. Perform milling or turning to provide the basic shape for subsequent processing. Quench and temper the mold material to increase hardness.
3. Assembly and debugging
According to the mold design, fix the C45 mold frame and cavity and core. Install the hot runner open gate system and test the stability of the injection system. Test the mold performance through the applicable 4000-ton injection molding machine, adjust the problem to ensure that the product size and weight meet the standard.
4. Injection molding production process
Dry the pure high-density polyethylene plastic to remove moisture. Set the appropriate injection pressure and temperature according to the mold size (1850x1300x1900 mm) and product weight (46 kg). After the trash can is formed by high-pressure injection molding, it is quickly solidified through a cooling system.
How to maintain
1. Clean the mold regularly
Remove debris, residual plastic and oil from inside and outside the mold regularly, especially waste materials in the gate system and cavity. The hot runner system needs to be cleaned regularly to avoid material blockage or runner damage.
2. Lubrication and maintenance
Regularly lubricate the moving parts of the mold (such as sliders and mold clamping parts) to ensure smooth operation and reduce wear. For parts that do not often contact plastic (such as the surface of the core and cavity), apply anti-rust oil or lubricating oil to prevent rust or oxidation.
3. Mold inspection
Regularly check the wear of the cavity and core. If scratches or wear are found on the surface, repair it.
4. Repair and replacement
Once cracks, gaps or other damage are found on the surface of the mold, welding or repair should be carried out in time to avoid further damage.
What Is Dimension of 770L wheelie bins?

Design For Product &. Mould

What Kind of Plastic To Produce 770Litres Bins?

How To Quality Manufacture 770L Plastic Wheelie Bin Mould?

Piece Is Taken By Robot After Molding
Package &. Delivery

Mould Components
Mould Steel
Hot Runner System
Standard Parts

FAQ
Q: How long does it take to make a set of mould of 770L Wheelie bins?
Q: Is it necessary to use a release agent while making mould?
Q: Can I reuse the mould?
Q: Do I need any special skills or equipment to make bins moulds?
Q: What are some advantages of making mould?
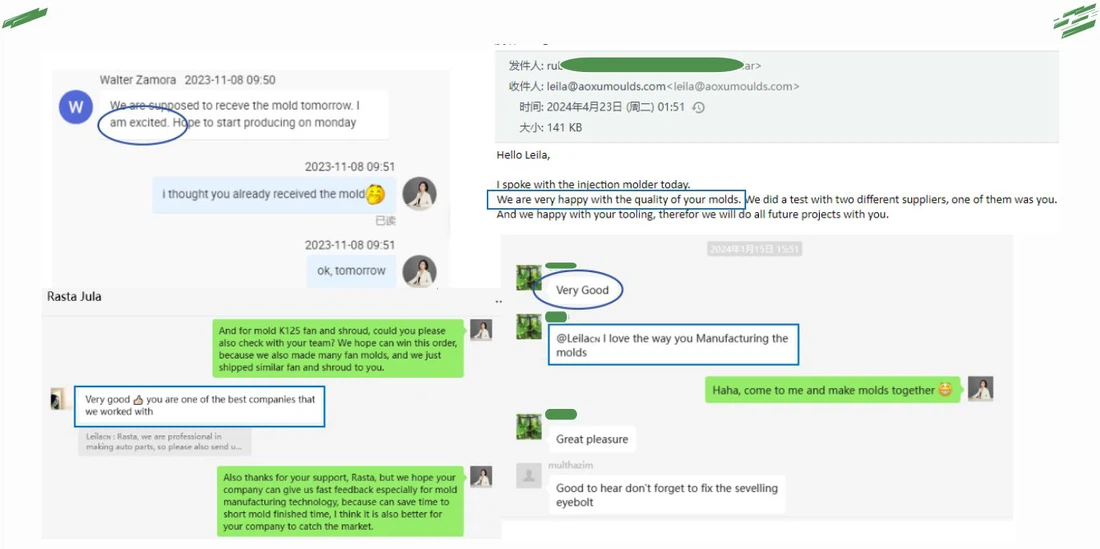
Customers' Feedback